Direct Answer
Locate the feature in the glass, on a face or at an edge, then compare it with the criteria for that zone under the agreed lighting and orientation. Use the dimensional, assembled-light or stress checks specified for the part, since a visual check answers only the appearance question. Record the observation, the suspected cause and the acceptance decision separately so that the next person can repeat the check.
Locate the feature before naming a cause
A glass shade can show a small dark spot when the fixture is off and a bright point when it is lit. A lens can show a faint ring on the inspection bench that becomes prominent after the retaining ring is installed. In each case the first description should say where the mark sits, which side faces the source, and how the mark changes with illumination or orientation. That description gives the designer, inspector and production engineer a common starting point.
Work from the outside in. Verify whether the mark follows the part when it is rotated. Check whether it comes into focus on the near face, the far face or within the wall, accounting for reflections from the two faces. An edge interruption can often be located by following the finished profile into the affected area. If the location is ambiguous, record it as unresolved and preserve the part for review under a suitable inspection setup.
Make the observation reproducible before debating its importance. A record such as “isolated point in the wall at the shoulder, seen with the source behind the part” gives the next inspector a location and a way to look for it. Add an orientation reference and a part identifier so the image can be compared with the drawing and another sample. When a photograph is used for scale, place the scale near the feature or use a calibrated image.
What common glass defects can look like
Bubbles, seeds and solid inclusions
A bubble is a gas-filled void. The term seed is commonly used for a small bubble, with any size boundary established by the applicable specification or agreed terminology. A solid inclusion is material embedded in the glass. It can appear dark, bright or nearly transparent depending on the inclusion and the viewing conditions. A rounded outline or the color of a spot can guide a first observation. Confirming the identity of the feature can require further examination. SCHOTT TIE-28 on bubbles and inclusions
For a suspected bubble, note whether it lies entirely within the wall or is open to a surface. Record whether the feature is isolated or part of a cluster and whether it lies inside the portion of the part that transmits useful light. Melting and refining are plausible investigation stages when bubbles recur across parts from the same glass supply. A repeat near one formed detail can justify checking the forming sequence as well. Keep that stage assignment provisional until part and process records support it.
An irregular point with a solid-looking center can be logged as a suspected inclusion. Some solid inclusions are described as stones. An unmelted particle or a fragment from material in contact with the melt may be among the hypotheses. The practical first question is whether there is a solid feature in the glass or a mark on a face. Keep the part and its lot identity if the answer could change disposition, and arrange material identification if the origin matters to corrective action.
Cords, striae and formed surface marks
Striae are local variations in refractive index within glass. They can appear as bands or streaks in a suitable transmitted-light setup. A cord can describe a streak-like inhomogeneity in glass. Agree on terminology before the same label is used for a line on the surface. For a streak in the apparent light path, check the part in transmission and then inspect each face separately. If the effect recurs through the bulk, the glass history and the applicable optical requirement are reasonable subjects for review. SCHOTT TIE-25 on striae
A formed surface mark can follow a tool split or a tool contact area. Some seam traces and patterns are expected at specified locations. A ripple described as a chill wrinkle is an appearance observation until the forming conditions have been checked. Container manufacturing guidance describes wavy areas associated with cold molds as one process-specific example. For a lighting part, compare the location across samples and evaluate the mark against the applicable appearance, profile and interface requirements. Bucher Emhart Glass container defect guide
A patterned lens or diffuser needs a baseline for the intended surface. An interrupted pattern at the perimeter, a scratch crossing the pattern and an expected change in relief near the rim are three separate observations. Agree which side carries the relief and where it should end. On a textured diffuser, check the affected region with the source in its intended position when the part’s lit appearance matters. The optical glass component range gives examples of how the surface geometry varies between diffusers and lenses.
A tinted diffuser disc with a specified texture illustrates the distinction. Inspect the expected pattern and the new mark under the same conditions used for the approved reference. A pattern interruption should be recorded by location and extent. An unusual bright patch in the assembled fixture belongs in a separate record of the lit result. That separation lets the project team decide whether the drawing needs a profile check, a visual limit or a lighting performance check.
Edge damage, uneven walls and residual stress
Inspect the edge where cutting, grinding or handling can leave chips or scratches. Record how far a feature extends along the edge and whether it enters the seating or sealing surface. For a crack-like feature, segregate the affected part for technical review against the project criteria and preserve its orientation. If a part has already broken, the fracture surfaces and the loading history can help a specialist investigate the origin. NIST guide to fractography of ceramics and glasses
Wall thickness is a geometric characteristic. Uneven thickness becomes a nonconformance when it falls outside the specified limits or fails a defined functional check. Two hollow shells can share an outside contour and differ at the shoulder or neck. In container blow-forming research, preform temperature distribution was examined as a factor in predicting the finished wall profile. For a lighting shell, agree the measurement stations on the section drawing and assess the readings against that part’s requirements. Giannopapa and Groot on glass container blow forming
Residual stress is stress remaining in the part after processing. The cooling history can affect the residual stress in glass. In an appropriate polarized-light setup, stress-induced birefringence can create a visible pattern. Pattern appearance depends on the optical path and the setup. If the project specifies a quantitative assessment, use a method suited to the part geometry and the specified quantity. Treat a normal-light appearance check and a stress check as separate entries in the inspection record. SCHOTT TIE-27 on stress in optical glass
Match each observation to a check
Use the table when deciding what to record and what to check next. A dark point, a wavy patch and an irregular rim can be visible in the same part. Write a separate entry for each feature and prioritize the area that controls fit or light. The right-hand column identifies the information needed to make a disposition. It can be a drawing requirement, an agreed appearance reference or a test of the component in its intended assembly.
| Observation | Possible location or stage | First check | Acceptance evidence |
|---|---|---|---|
| Bubble or seed | Enclosed or surface-open void. Review melting, refining or forming as indicated. | Locate it. Record size, distribution and zone using the agreed method. | Drawing or visual limit. Lit check where specified. |
| Solid inclusion or stone | Embedded material. Review the glass supply and melting history if the pattern supports it. | Separate bulk and surface observations. Preserve the sample for identification. | Agreed inclusion criteria and the requirements for that zone. |
| Cord or stria | Bulk optical inhomogeneity if confirmed in transmission. | Locate the streak relative to both faces. Compare with the optical reference where specified. | Applicable optical drawing requirement or agreed assessment. |
| Seam trace or ripple | Tool split, contact or thermal history during forming. | Compare repeat locations and the finished surface profile. | Agreed appearance limit, interface dimension or fit. |
| Chip or scratch | Edge or face. Compare finishing and handling history. | Locate, record extent and identify any overlap with the seating zone. | Edge or surface criteria and any applicable fit check. |
| Wall-thickness variation | Section geometry and material distribution during forming. | Measure the specified stations on the finished part. | Drawing limits and any specified functional check. |
| Stress-related pattern | Possible residual stress after the thermal history of the part. | Use the agreed polarized-light method if stress assessment is required. | Specified result, method and acceptance requirement. |
Specify the part zones and the viewing conditions
Draw the functional zones
Mark the usable light-transmitting area, the visible surround and the seating or sealing region on a drawing view that both parties can orient. Include a section through an interface if the top view alone leaves its boundary ambiguous. The same size of mark can have different implications in those areas. A point inside the usable aperture can warrant a light check. A protrusion in a concealed seating zone can warrant a fit check. A mark on the exposed surround may be evaluated against an appearance reference.
Consider a domed optical lens with a stepped mounting neck. The dome and the mating neck serve different functions. A drawing can identify the transmitting face, the locating diameter and the glass surface that contacts the fixture. For a custom lens drawing, dimension the mounting interface and specify where any surface or edge imperfection would affect engagement. The measured profile and the fit in the holder should be assessed against the agreed revision.
For an optical project that calls for ISO drawing conventions, ISO 10110-18 addresses indications for internal optical material imperfections, including bubbles and inclusions, striae and stress birefringence. ISO 10110-7 addresses surface imperfections in a specified test region of finished optical elements and assemblies. Choose the applicable convention and define the required level for the individual part. A decorative shade may instead use a project-specific visual agreement and separate dimensional requirements for its mounting edge. ISO 10110-18 and ISO 10110-7
Agree how the part will be viewed
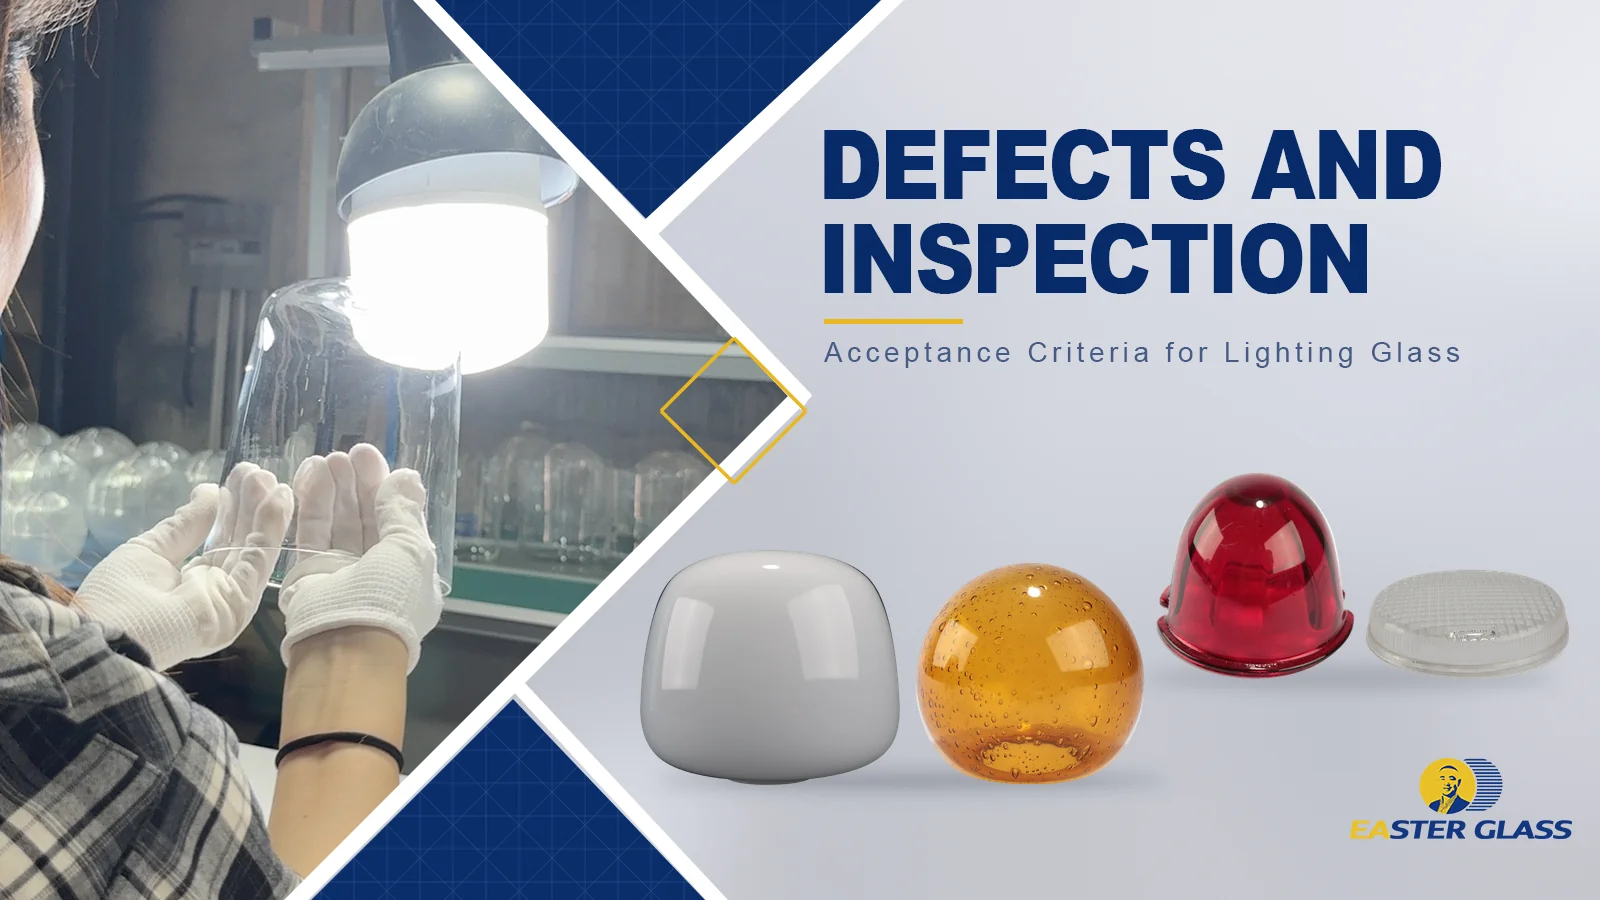
Use a clean part and describe the light direction, background, viewing distance, orientation and inspected side. Transmission with the light behind the part can make features inside the wall easier to locate. Oblique illumination with the light to one side can make fine surface marks easier to see. A steeply curved part can create reflections that shift when the part is turned. Change one condition at a time and return to the agreed setup for the acceptance observation.
When the inspector and the lighting designer judge the same sample under different conditions, both records can be relevant. Use the bench setup for repeatable appearance decisions. Use the specified holder, source position and operating state for the agreed lit check. A point that is visible on the bench and a visible bright spot on a diffuser belong in related entries with distinct conditions. Record any change in source, part orientation or holder between samples.
For a custom glass sample approval, record the drawing revision, viewing method and sample identifier together. If the project uses a limit sample, label the zone and the feature that it defines. Specify the applicable count, size, spacing or comparison criteria when those distinctions are needed. Easter Glass’s quality and inspection overview describes using approved drawings, reference samples and agreed inspection scope for finished parts. The part-specific limits come from the project documents.
Trace recurring marks to a process stage
Compare the pattern across parts
Plot the same feature on several parts using the same datum. A mark at the same clock position relative to a split line or mounting feature suggests a location worth checking on the tool or fixture. A mark that moves around the part but appears within one lot suggests a different comparison, such as glass supply or shared handling. Rotation is only meaningful if the orientation reference is consistent across parts. Record the lot, date and cavity or tool identifier when available.
For a blown glass shade manufacturer, a recurring line near the shoulder might be investigated by comparing parts from different tools or runs and tracing which operations share that region. For a pressed glass lens supplier, a mark repeated beside a locating feature might be compared with the tool contact and any finishing fixture. Inspect samples before and after the suspected operation when such samples are available. Easter Glass’s lighting glass forming overview explains where forming and later finishing fit in the process chain.
Keep an open hypothesis when the evidence points to several stages. For example, two lots may share a finishing fixture even if their forming tools differ. A repeated edge mark on both lots could justify examining the finished-edge handling sequence before changing the forming settings. Conversely, if the feature is visible before the first finishing step, compare upstream samples and process records. Record which observation would support or rule out each candidate source.
Tie prevention to a confirmed stage
When a surface mark has been traced to a contact point, review the contact surface, part orientation and handling sequence with the production engineer. When a thickness issue occurs across a particular section, review the shape, forming conditions and the repeatability of the measurement at that station. When the team suspects residual stress, review the thermal history and the agreed verification method before changing the process. Preserve a comparison sample so the corrective action can be checked against the original symptom.
For a glass diffuser production partner working on a repeat order, an approved appearance sample can help maintain a stable reference across teams. Add an independent fit or lit check where the appearance result cannot answer the functional question. During OEM lighting glass development, document which characteristic is controlled by the drawing, which by the sample and which by the assembled fixture test. This allows later changes in the source, holder or glass geometry to trigger the appropriate review.
Worked example for a glass globe and retaining ring
Suppose a blown globe shows a faint line around part of its neck. On the bench, a side light makes the line easier to see. Mark the clock position relative to the holder orientation and compare the profile at the neck with the finished drawing. Then fit the globe into the holder using the specified retaining parts. A line that appears on the visible neck and a ridge that interrupts seating need separate observations, even if both originate near the same tool feature.
If the globe seats correctly but the line remains visible, compare it with the agreed reference from the specified viewing position. If the globe rocks or touches the ring at one point, record the contact location and measure the relevant mating surfaces. A pressed part with a similar-looking line would follow the same sequence of questions, while its likely manufacturing sources would be evaluated against its own operations. A decision to accept, segregate or request more evidence should identify the exact requirement applied.
For made-to-drawing glass covers, make the evidence package small enough to repeat. Include one orientation view, one close view of the feature, the drawing revision and the specific measurement or functional check that resolved it. Preserve the original samples when a batch or process investigation is open. A reviewer can then distinguish the reason for the current disposition from the additional work needed to prevent recurrence.
Technical Takeaway
Define the acceptance conditions for each critical zone before comparing samples. When a new mark appears, locate it, record the observation conditions and choose a check that answers the function of that zone. Use repeat position, process sequence and lot records to narrow the likely source. Record the evidence and the applicable criterion with the disposition so a second reviewer can reproduce the decision.
Frequently Asked Questions
Is every bubble in a glass lamp shade a defect?
A bubble is an observable feature. Its acceptance depends on the project criteria, its location, its size or distribution and any agreed light check. An enclosed seed in a concealed portion of a shade and a cluster in the part’s usable light path may be assessed against different requirements.
How can I tell a scratch from a streak inside the glass?
Compare the same area using oblique illumination and transmitted light. Try to locate the feature relative to each face by changing the viewing angle or focus. If the location remains unclear, record it as unresolved and review it using the agreed inspection method before assigning a cause.
Can visual inspection verify residual stress?
Ordinary appearance inspection records features seen under the agreed viewing conditions. A suitable polarized-light method can reveal stress-related birefringence. Where the drawing requires a quantitative result, specify the method, geometry and reporting convention before using the result for acceptance.
Review a lighting glass inspection requirement
Send the drawing revision, the part orientation, the affected zone and photographs with the lighting conditions noted. If the issue appears in assembly, include the mating part or fixture details and the criterion that needs to be checked.
Share the drawing and inspection details
Technical note
The illustrations and worked example are schematic. Apply the inspection method, viewing conditions and acceptance criteria defined for the actual part and its intended application.
 English