What does cold working mean for a lighting-glass part?
The Corning Museum of Glass uses cold working as a broad art-glass term for techniques that alter or decorate glass when it is cold. The museum’s definition includes actions such as engraving and cutting, so it is wider than the industrial finishing question addressed here. In this article, the working scope is material removal and surface or edge finishing on a glass component after forming.
That scope includes grinding, polishing and the finishing of an edge, rim, opening or other surface when a part drawing requires it. It does not mean that every formed glass part needs a secondary operation. A molded contour may already provide the required geometry; a different part may need a local feature changed to establish a fit, a reference surface or a specified appearance. The drawing and the approved sample determine which state is intended.
“Cold” distinguishes these operations from working glass while it is soft enough to be shaped by heat. It does not mean that the glass is refrigerated. Fire polishing is also separate: the Corning Museum describes it as using heat to soften the surface. Mechanical grinding and polishing remove material through contact or reaction; fire polishing changes the surface through heating. A broader overview of forming routes appears in the lighting-glass forming process overview.
How do grinding and polishing remove glass?
General industry reference, precision-optics fabrication, principle only; not a conclusion about lighting parts and not a description of Easter Glass practice. Lehigh University’s glass-processing lecture, prepared by a Lawrence Livermore National Laboratory researcher, explains grinding and polishing as interacting material-removal mechanisms. The actual result depends on the material and process conditions; the lecture is not a recipe for a lighting component.
In the lecture’s brittle-removal model, abrasive contact removes glass around lateral cracks. That removal can leave scratches and damage below the visible surface. The visible scratch is therefore not a complete description of the altered material. A drawing or appearance review that only names “polished” does not establish the subsurface condition or prove that a part meets a functional requirement.
The same teaching material distinguishes plastic, or ductile, removal from brittle grinding. In that regime, part of a deformed region is removed, and fine plastic scratches can remain. It also describes chemical polishing as molecular-level removal through a surface reaction. These mechanisms are presented as precision-optics principles; they should not be read as a statement that a given lighting-glass edge is produced by one of them.
In an optical-fabrication sequence, each later step is intended to address the deepest damage left by the preceding step, while the removal rate becomes lower. That is a process-design principle from the lecture, not a mandatory step list or a promise of a particular finish. A component may need no polishing at all, and the target surface may be decorative, mechanical or optical rather than a precision optical face.
| Mechanism | What the reference describes | Why it matters to interpretation | Scope |
|---|---|---|---|
| Brittle removal / grinding | Material around lateral cracks is removed; scratches and subsurface damage can result. | A visible surface can look different from the damage left below it. | General industry reference, precision-optics fabrication, principle only. |
| Plastic / ductile removal | A portion of deformed material is removed; fine plastic scratches, sometimes called sleeks, may remain. | The word “polish” alone does not identify the resulting surface or its acceptance. | General industry reference, precision-optics fabrication, principle only. |
| Chemical removal | Material is removed through a surface reaction at the molecular level in the described polishing model. | This is a different mechanism from abrasive contact and should not be inferred from a finish label. | General industry reference, precision-optics fabrication, principle only. |
| Step-to-step damage removal | Later steps target the deepest damage left by earlier steps and remove material at a lower rate. | A sequence is selected for a stated surface objective; it is not universal. | General industry reference, precision-optics fabrication, principle only. |
| Abrasive contact conditions | The lecture relates the removal mechanism to the particle or tool contact and its loading. | No force, grit, depth or speed value is transferred to a lighting part here. | General industry reference, precision-optics fabrication, principle only. |
The Lehigh University glass-finishing lecture is the source for this mechanism summary. General industry reference, precision-optics fabrication, principle only; not a conclusion about lighting parts and not a description of Easter Glass practice. No force, particle size, scratch depth or other numerical process value is quoted here.
Why does the glass material matter?
General industry reference, precision-optics fabrication, principle only; not a conclusion about lighting parts and not a description of Easter Glass practice. SCHOTT’s technical information on optical glass states that hardness and grindability influence the process needed to achieve good polishing quality. The same document cautions that grinding behavior depends on multiple conditions and is not characterized by one single material property. This is an optical-glass reference, not a ranking of lighting-glass compositions.
The practical implication is modest but useful: a process label cannot replace a material specification and a stated surface objective. “Glass” is not one interchangeable grinding response. Composition, the part’s shape, contact area, tool and abrasive conditions, and the required surface all matter to process planning. The reviewed source does not provide a transferable recipe for a lamp shade, globe, diffuser or mounting rim.
SCHOTT’s separate discussion of precision molding provides a bounded example. For a particular reheat-pressed optical-glass route, the pressings have a rough surface and need additional grinding and polishing. The described precision-molding route instead starts with a prepared preform whose surface quality is intended to be conserved. These are two optical-lens routes; they do not prove that a molded lighting component generally needs polishing, or that a particular finish is available from Easter Glass.
The references are useful because they show why the material and the forming route belong in the same review. The Borosilicate Glass collection and the Optical Glass collection organize different product families; they are not cold-working process specifications. For a custom lighting part, record the specified material separately from the operation and finished surface being requested.
See SCHOTT TIE-31, Mechanical and Thermal Properties of Optical Glass, and SCHOTT TIE-40, Optical Glass for Precision Molding. Both are optical-glass references. No numerical material or process values from them are applied to lighting components in this article.
Where can cold working sit in the manufacturing chain?
Cold working follows the creation of a glass form, but that statement does not define one fixed sequence. A formed component may be accepted as formed, or a drawing may require a later operation on a specific face, opening, rim or edge. The sequence must match the material, geometry and downstream process. General industry reference, precision-optics fabrication, principle only; the examples below do not describe an Easter Glass production route.
| Process context | What the cited reference says | Boundary for a lighting project |
|---|---|---|
| Molded seam | The Corning Museum’s glass dictionary says seam marks indicate mold-making and that well-made art-glass pieces may have them smoothed by grinding or fire polishing. | This definition does not establish that every mold trace should be removed from a lighting part. |
| Reheat-pressed optical glass | SCHOTT describes a specific optical-glass route whose rough pressed surface needs additional grinding and polishing. | Keep this as an optical-lens example; do not generalize it to all pressed lighting parts. |
| Precision-molded optical preform | SCHOTT describes a prepared polished or fire-polished preform whose surface quality is intended to be retained during molding. | The route is specific to the documented optical process and is not an Easter Glass capability statement. |
| Fire polishing | The museum defines fire polishing as using heat to soften the surface. | It is a separate heat-based process, not mechanical grinding or cold polishing. |
The process chain should be read from the final part backward. Identify the surfaces that locate the part, touch a fixture, seal an opening, transmit or redirect light, or remain visible after assembly. Then establish which route forms each surface and whether any later operation is specified. A general statement such as “finish the edge” is not enough when the edge also establishes a seating position or defines the entrance to a light path.
A broad concept map is available in the published overview of forming processes for lighting components. This article narrows the question to post-forming removal and finishing. It does not restate the process boundary for thermally tempered flat glass; that sequence must be checked against its dedicated, approved technical guidance before a flat part is specified.
How should an edge or finished surface be specified?
Begin with the edge’s function. An opening perimeter may be visible, may contact a retaining component, or may define clearance around a light source. A different edge may only close an outline. A face may be decorative, or its geometry may control how light passes through the part. The same word—“polished”—can therefore refer to different acceptance questions. State what the surface must do before choosing a finish label.
For a seating interface, show the mating hardware or provide a representative sample. Identify the contact band and the feature used as the drawing datum. For a visible edge, define the viewing side and the reference appearance. For an optical zone, identify the active area and describe the optical or lit check required by the design. Keep each requirement tied to a part feature rather than applying a broad finish description to the whole component.
A finish term is not a substitute for the finished geometry. If material removal changes an opening, the drawing should identify the final opening and the adjoining locating feature. If the design needs two ends to align with a fixture, specify their relationship and the state at which it will be checked. If the surface has a visual requirement, use an approved comparison sample or a project-defined observation condition. Do not add a roughness value, dimensional allowance or inspection limit unless the project evidence supplies it.
Edge names can vary among product families and suppliers. This article does not rank edge profiles or present a universal list of finished-edge types. It also does not explain or recommend CNC glass edge processing: the reviewed technical references do not substantiate a machine-controlled edging method for the lighting parts discussed here. A drawing should describe the geometry, location and function that must be achieved; the process route should be confirmed against the specific part evidence.
A practical review separates four things: the original formed surface, any surface to be removed, the final interface, and the evidence used to accept the part. This makes it easier to see whether a requested change is a cosmetic treatment, a geometric adjustment, or a function-critical feature. It also makes a sample review more useful: the team can compare the same surface and assembly condition instead of relying on an undefined “smooth edge” description.
Define the area and function.
Identify the mating surface and datum.
Specify final geometry and viewing state.
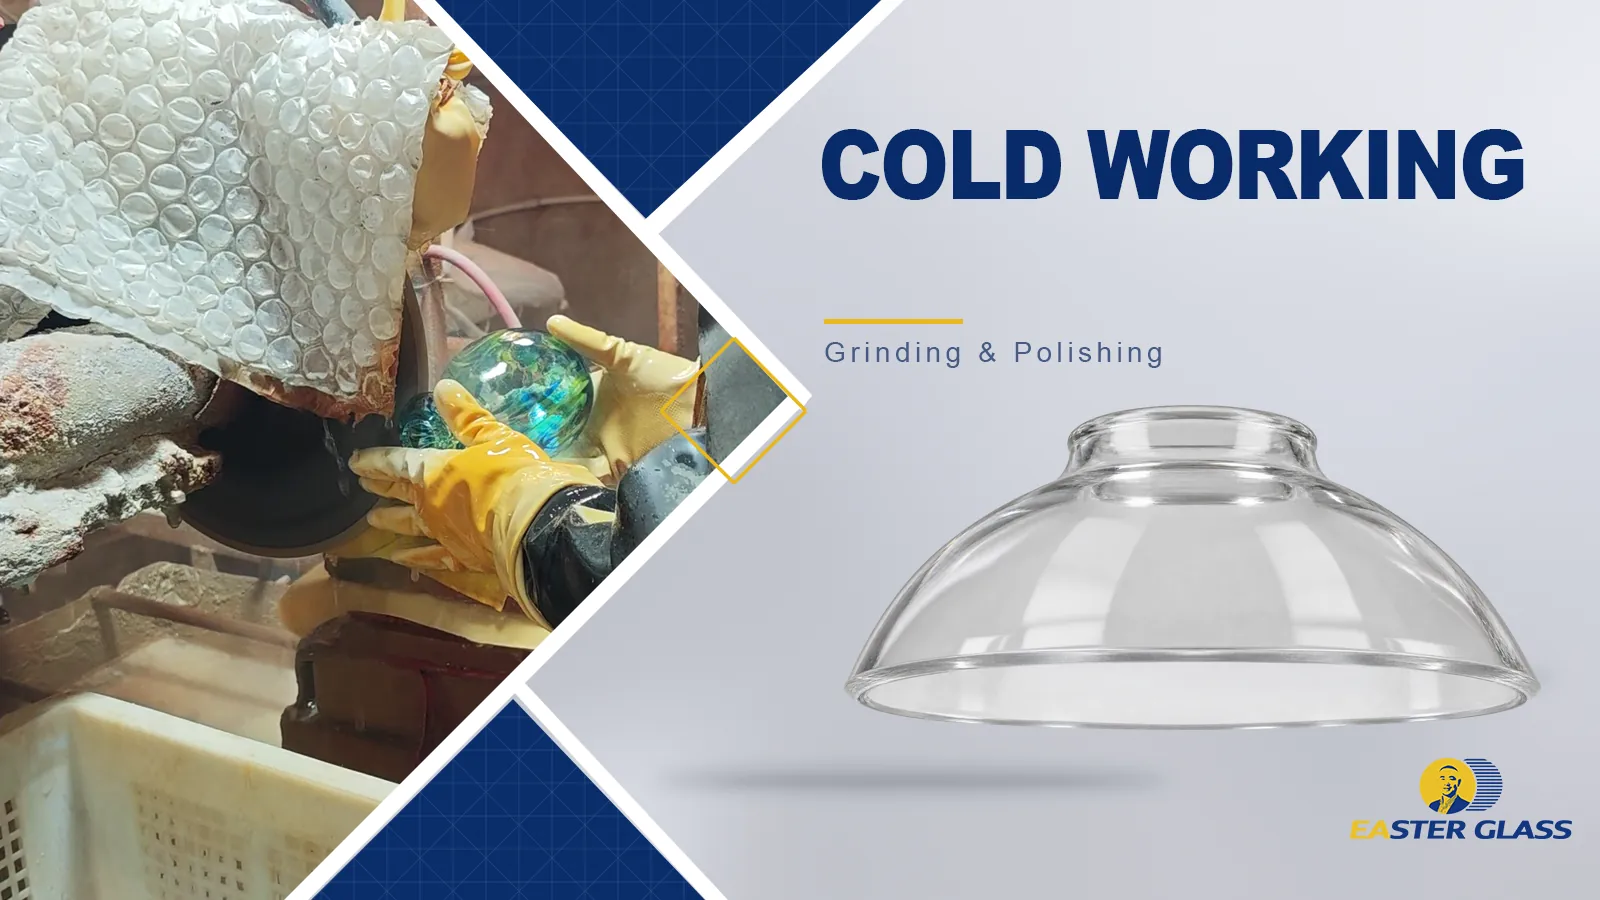
A company video that shows a cold-working step
The official Easter Glass clip below shows cold working on a formed borosilicate component. It is a direct visual example of a secondary operation on one component. It does not show every removal mechanism described above, identify the exact operation or equipment, establish a finish limit, or prove that the same route applies to the linked product examples.
Which drawing inputs help define a cold-working requirement?
A custom part drawing should make the intended finished condition understandable before a process is selected. The purpose is not to prescribe equipment from a blog article. It is to let the glass designer, manufacturing reviewer and lighting engineer discuss the same feature using the same sample state. The table below is an engineering-input guide, not an Easter Glass production checklist or a guaranteed service scope.
| Input | Question to answer | Why it matters |
|---|---|---|
| Part form and feature location | Which opening, rim, face or perimeter is involved? | A process or finish term without a location can refer to the wrong surface. |
| Material specification | Which glass composition or approved material family is intended? | The optical-glass references do not establish behavior for every lighting glass. |
| Functional zone | Does the surface locate, retain, seal, clear a component, transmit light or remain visible? | The function determines which evidence is relevant for review. |
| Mating hardware and assembly state | Which ring, holder, seal or light engine contacts or passes through the glass? | A finished edge can be judged in the actual interface rather than by appearance alone. |
| Finished-part datum and dimensions | Which final feature locates the part, and when is it measured? | Measurements before and after material removal may describe different part states. |
| Acceptance evidence | Is the requirement checked by a drawing dimension, sample comparison, fit check or optical review? | The method should answer the requirement rather than substitute for it. |
For a lighting part, quantity and project stage can also affect how a design is reviewed. A first sample may answer whether the component seats or clears an assembly. A later sample may be needed to judge appearance in the intended light. These checks are different from proving a controlled optical surface. State which question the sample must answer and identify the drawing revision and mating parts used for that review.
A surface requirement should also identify the state being compared. A component measured before finishing may not share the same edge geometry or datum as the final part. Record whether the drawing, sample photograph and physical sample represent as-formed, intermediate or final conditions. If a light-transmitting face is evaluated after polishing, keep the source position, assembly orientation and viewing method consistent. Otherwise, the comparison may mix a finishing change with a change in the test setup. Keep a clean sample and drawing revision available whenever acceptance depends on assembly fit.
The Easter Glass Quality page is the site’s owner page for quality and inspection information. A project-specific acceptance limit, test method or inspection record still needs to be confirmed for the part; this article does not assign any such limit.
What do published lighting-part examples show?
Current Easter Glass product pages show why an edge requirement should be attached to the component drawing. The page for a clear chevron globe shade with a cut opening and ground rim describes the finished opening as part of its mounting area. The page for a gradient frosted borosilicate tube shade with two ground ends identifies the tube ends and stepped seat as part of the interface. A coral petal shade with a scalloped cut and ground opening illustrates a shaped perimeter rather than a simple circular rim.
These are examples of product-page descriptions, not process records. They do not identify the machine, abrasive, finishing sequence, inspection limit or whether an operation is performed in-house or by a partner. A product detail page can help a reader picture the part geometry; its stated edge condition should not be generalized into a universal manufacturing method.
For a project discussing a manufacturer of glass globe shades with drawing-defined ground openings, the useful technical input is the section view, the final opening geometry and the mating hardware. For a supplier of borosilicate tube lamp shades with fixture-mating ground ends, the drawing should also distinguish the end condition from the tube’s visible or functional face. These phrases describe specific engineering contexts; they do not claim a particular process route.
When a drawing or physical sample is the starting point, an lighting glass development partner for drawing-defined polished optical faces needs the functional zone, material, assembly arrangement and acceptance evidence to be reviewed together. Easter Glass’s OEM/ODM page describes development around drawings, samples or project concepts. It does not establish that every requested grinding or polishing operation is available for every design.
To assess surface marks or edge damage, the published lighting-glass defects and inspection article covers observation and acceptance boundaries. CP-24 stays with the cold-working mechanism and specification inputs; it does not diagnose a crack, assign a defect cause or set a pass/fail rule.
Easter Glass develops custom lighting-glass components on an OEM and ODM basis. The approved source set for this draft does not verify which cold-working operations are performed for which parts, what equipment is used, or whether any operation is carried out in-house or through a partner. Those details are intentionally not presented as company capabilities here. Confirm them for the specific part before describing a production route or making a process commitment.
Technical Takeaway
Treat grinding and polishing as process names, not finished-part criteria. Define the glass, the surface or edge, its function in the lighting assembly, the final datum and the evidence used for acceptance. Use precision-optics sources for their stated scope, and do not turn their mechanisms or process sequences into an unverified specification for a lighting part.
Frequently Asked Questions
What is cold working of glass?
It is a broad term for techniques used to alter or decorate glass after it is cold. The Corning Museum of Glass uses it broadly in an art-glass dictionary. In this article, the term is narrowed to grinding, polishing and edge finishing for formed glass components.
What is the difference between grinding and polishing glass?
In the precision-optics teaching material cited here, grinding is associated with brittle removal and possible subsurface damage. Polishing describes finer removal mechanisms that address the surface left by previous steps. This distinction explains a process principle; it does not define a universal lighting-glass finish.
Why can grinding leave subsurface damage?
Abrasive contact can remove material around cracks that extend beneath the visible surface. The surface can therefore look different from the altered region below it. The depth and acceptance of any damage are not specified for lighting parts in this article.
Why might a molded glass part need grinding or polishing?
A molded part may need a later operation if the drawing requires a changed edge, opening or surface. A museum definition notes that mold seams on art-glass pieces may be smoothed, and SCHOTT describes one optical-glass pressing route that needs additional grinding and polishing. Neither example means every molded lighting part requires that work.
Do all glasses grind and polish in the same way?
No. SCHOTT notes that optical-glass grinding depends on multiple conditions and is not characterized by one property alone. The cited documents do not provide a general ranking for lighting glass, so the material and required surface must be reviewed for the specific part.
Review a drawing-defined glass edge requirement
Share the drawing or sample, material requirement, mating hardware, intended function and acceptance question. The OEM/ODM development page explains how a lighting-glass project can be reviewed from its design inputs.
Easter Glass develops custom glass components for lighting projects on an OEM and ODM basis.
Technical note. The diagrams are conceptual. External sources describe glass definitions and precision-optics mechanisms within their stated scope; they do not establish an Easter Glass process setting, capability, equipment, inspection method or acceptance limit. Confirm each requirement for the actual part and its intended application.
Custom glass components for lighting projects.
 English