Direct Answer
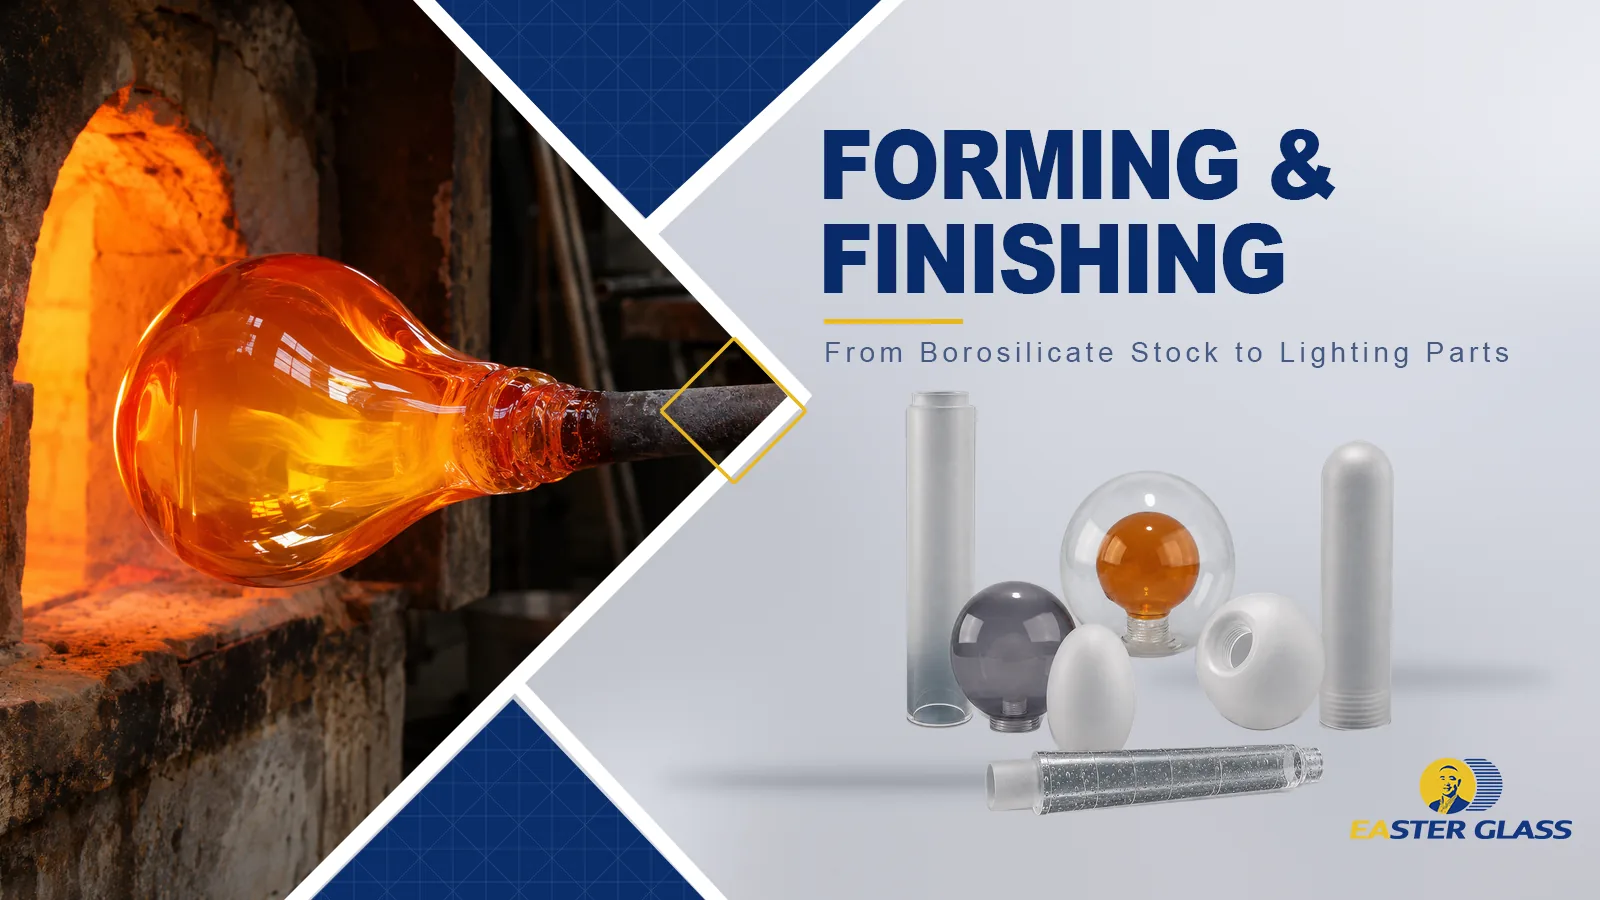
Borosilicate lighting components can retain the main section of a tube or flat blank, take on a new section when glass is reheated and reshaped, or receive their form in a mold. The design review starts with the stock and the finished section drawing. Identify which operation establishes each opening, seating face and optical surface, then check those features on the finished part in the intended mounting condition.
What does the starting glass form tell you?
Specify material and stock separately
Borosilicate identifies a family of glass compositions. Tube, rod and sheet describe the geometry supplied to the next operation. For example, a tube has an inner and an outer surface, a rod begins as a solid section, and a sheet provides two broad faces with a defined thickness between them. Each form leaves a different set of surfaces available for cutting, finishing or reshaping. A grade specification belongs on a separate line of the drawing or material schedule. For a reference on the scope of a specific grade, see ISO 3585 on the properties of borosilicate glass 3.3.
Ask which surfaces the finished part inherits from the stock. A straight tube shade can carry the original bore along most of its length. A flat cover may retain the original faces over its aperture while an edge is cut and finished to fit the frame. In a mold-formed part, the forming route establishes the initial surfaces of the relief or shell. Reheating already formed glass for downstream operations is an established approach, illustrated in SCHOTT's overview of converting and reshaping.
Read the finished section before choosing a route
For a simple tube, specify the outside diameter where it locates in the holder, the bore where it clears the light source or another component, and the length between the relevant end faces. Where these dimensions interact, show the position of each measurement on the drawing. An enlarged shoulder, a reduced mouth or a change in wall section can introduce an additional inspection region. For examples of how a named tubing family describes outside diameter and wall thickness as separate stock variables, see the SCHOTT DURAN tubing and rod guide.
For a nominal circular tube with concentric walls, the bore diameter is the outside diameter minus twice the wall thickness. That relationship helps screen a stock size. For the assembled part, check the minimum clear opening where the mating item actually passes. An out-of-round opening or a local change in wall thickness can alter the clearance even when the stock’s nominal outside diameter is suitable. On a sleeve with an inserted module, define the maximum envelope of the module and the required clear path through the glass. The review may need measurements at both ends and at a formed transition.
A starting tube can also become a part whose main section is no longer tubular. A rounded enclosure with a short neck, for example, needs sections through the body, the shoulder and the neck. The wall and opening of the original tube provide information about the input. The revised geometry calls for its own finished-part criteria. Review any thickness distribution that affects clearance, fit or light transmission at the locations where that function matters.
Sheet stock provides a separate route for a planar window or cover. The outline, edge and any opening can be defined around the retained faces. Specify which face is exposed and where the frame bears, and leave the choice of cutting and finishing method to the project review. SCHOTT documents custom cuts and edge processing for a named flat product in its BOROFLOAT 33 general information.
| Stock and route | Features to establish | Drawing and first-article check |
|---|---|---|
| Tube retained | Cut length, opening edge and any local locating detail. | Bore, outside diameter at the seat and finished end faces. |
| Tube reheated and reshaped | Body transition, neck or altered opening. | Local section, clear path for assembly and final interface. |
| Sheet retained as a planar blank | Outline, finished edge and any required aperture. | Thickness, edge condition, frame contact and visible face. |
| Mold-formed glass | Shell or lens relief and its relationship to the perimeter. | Functional surface, mounting datum and finish on the approval sample. |
Which operations change the part after the stock is made?
Local hot work changes the section
Local hot working softens a selected region of the glass so its shape can change. That region may become a shoulder, an expanded body or a narrower opening. As the glass moves, the local wall distribution can change along with the outer contour. Put the opening and the transition in the same section view so the review team can see where a change in one feature might affect the other. The Corning Museum of Glass flameworking demonstration shows the general principle of heating rod or tube stock before shaping it.
It is useful to mark the areas of a drawing as retained stock geometry, shaped geometry and finishing allowance. A stock diameter can guide the initial selection when much of the tube will be retained. A formed neck needs its own internal and external dimensions at defined locations. If an opening will be trimmed or an end ground after forming, show the final face and its relationship to the locating feature. For broader context on how the forming route sets the original section, see the Easter Glass overview of glass forming for lighting components.
Follow the opening through the assembly sequence. A neck can suit the final holder but still limit access for a wider internal module or a tool. Identify the direction in which each item enters and the smallest cross-section it must pass. For an opening on a curved shoulder, show its orientation and the surrounding wall in section. This gives the forming review the relationship between the opening, the adjoining glass and the space available for later operations. It also gives the assembly team a view they can use when approving the first sample.
Finish and inspect in a defined sequence
Cutting separates a part or sets its length. Grinding can bring a cut edge or face to an agreed condition. Flame polishing uses heat at the surface and can change the local edge shape. Where an edge both finishes an opening and locates the glass, define the condition in which it will be measured. An as-formed edge and a final ground end represent different stages, so record the intended edge treatment in the drawing alongside the relevant size. See the Corning Museum of Glass definition of fire polishing for the principle of smoothing a surface with heat.
Consider the area available to finish an edge near a step or a tight transition. A face that looks accessible in a plan view can sit inside a recess when viewed in section. If it carries the assembly load, give the extent of the bearing surface and the edge condition that applies around it. Where a decorative finish reaches the same region, mark where it may end and which contact surface needs a defined condition. Record the finish boundary on the same revision as the mechanical interface.
The thermal history matters when the route includes hot shaping or later reheating. Plan the appropriate cooling sequence, including annealing after hot forming where applicable, and any agreed stress check for the geometry actually produced. A trial made from a straight tube represents different sections from a trial with a wide body and a narrow neck. Use a representative sample of the finished configuration when the geometry or the finish changes. Keep the material grade and relevant processing stage in the sample record so the results can be traced.
See tube stock being shaped
The Easter Glass process video shows localized flame heating and shaping of borosilicate tube material. The section changes around the heated region while neighboring material retains its original form. Use the footage to see how a tube becomes a part with different sections along its length. The drawing and approval sample establish which operations and inspection criteria apply to a specific project.
How do three finished parts change the drawing review?
Stepped tube shade with ground ends
The gradient-frosted borosilicate tube lamp shade has two open ends, ground ends and a stepped upper seating feature. Most of the body retains a cylindrical profile. In a review with a manufacturer of stepped borosilicate tube shades for pendant luminaires, identify the surface that carries the shade and dimension the installed length from it. If a collar guides the upper end, give the collar clearance and state the location at which the glass outside diameter will be checked.
Place the visual finish on a drawing view that shares the installed orientation. A gradient band has a position relative to the holder, and part of that band may be hidden once the shade is seated. Establish a reference for the visible length and a viewing condition for the transition. The Easter Glass Borosilicate Glass collection for tubes, shades and covers shows several shapes within the material family. Each needs its own location for the mounting and appearance checks.
Shallow oval cover with a raised rim
The clear oval borosilicate cover with a raised perimeter rim has a shallow curved body and an open underside. Its published process is precision pressing. A design review with a supplier of clear oval borosilicate covers for gasketed luminaires can use this geometry to define the intended contact band. Show the outline of the gasket and the rim in the same view, then give sections through the ends and sides where the contour or the contact condition differs.
The nominal oval outline provides overall clearance. A section through the rim establishes which face locates against the assembly. For a project with a gasket, include the housing reference surface and the intended compression or contact requirement from the assembly specification. This allows a fit check to distinguish interference at the outer rim from the condition on the bearing face. Check the completed joint if the project specifies a sealing performance requirement.
Pressed Fresnel profile with a frosted surface
The frosted borosilicate Fresnel lens with concentric steps is listed as precision-pressed. Its visible relief and perimeter rim present different design tasks. With a factory pressing frosted borosilicate Fresnel lenses with perimeter mounting rims, specify which drawing features belong to the optical relief, which face seats in the holder and where the finish applies. Define how the lens orientation will be preserved through measurement and installation.
The relief can be inspected for the agreed geometry, and the rim can be checked for fit using the intended datum. Evaluate the lit appearance or photometric output in the specified assembly when that outcome is required. Changes to the surface finish can affect the appearance of the relief under light, so the sample used for that approval should carry the intended finish. See the Easter Glass Optical Glass collection for other lens geometries for related examples of functional glass surfaces.
If both faces of a molded lens are functional, show each one in section with a clear source side and exit side. Give the orientation of the drawing relative to the installed light source. For a geometry comparison, keep the surface profile and rim measurements associated with the same sample. If an optical discrepancy appears, this record helps establish which parts share the same geometry, finish and mounting condition before the distribution result is interpreted. For the process considerations behind molded optical relief, see the Easter Glass guide to pressing lighting lenses and prisms.
What should the drawing and first article show?
Link dimensions to the actual assembly
On a single drawing revision, identify the material requirement, expected section, mounting interface and finished visible surface. Assign each critical dimension to a named face, axis or position along the part. A shoulder height measured from a cut end can differ from the installed height measured from the seat when the end is free inside the housing. For made-to-drawing borosilicate lighting covers, supply the mating section or assembly drawing so the inspection reference matches the function.
For custom borosilicate tube shade prototypes, check where the holder contacts the glass, which end enters first and whether the edge finish changes the clearance. If a thread, clip or collar locates the part, include the relevant mating component in the fit check. Separate the measurement of a feature from the trial that confirms it assembles. The drawing review, prototype and approved sample sequence is described in the Easter Glass OEM/ODM development process.
Use a trial that can distinguish contact from interference
Consider a stepped shade that enters its collar by hand but sits at an angle after the fixture is assembled. Inspect the ground end and the step against the section drawing, then compare them with the holder and its intended seating surface. Record where the glass first touches during insertion and where it rests once secured. If a nearby edge touches early, compare that edge clearance with the target seat height before deciding which dimension needs attention.
If the next sample changes the length of the neck or the finish of the edge, use the same mating part and orientation for the comparison. Record the measured position of the step, the location of contact and the finished shade’s installed height. A trial that repeats these checks can show whether the change resolved the interference and whether the visual band still falls in the intended part of the fixture. Preserve the drawing revision and the sample state alongside that result.
When the mounting parts themselves vary, record which holder the trial used. A shade can seat correctly in one collar and encounter a different clearance in another. Use the drawing’s intended mating dimensions to decide whether to check additional holders or specified limit conditions. If the team adjusts a contact face, recheck the visible gap at the fixture and the position of the lit band, because the same face can establish both the mechanical position and the apparent height of the shade.
Define the acceptance state before the process is fixed
For an OEM drawing review for pressed borosilicate optics, state whether the geometry check is on the formed piece or on the finished lens, and state where the assembly verifies the seating face. If the project has a lit appearance or light-distribution requirement, identify the source, lens orientation, reference assembly and the agreed method. A sample with the specified finish connects the dimensional record to the functional evaluation. For context on matching the inspection plan to the part, see Easter Glass lighting glass quality and sample review.
Where the assembly will see significant temperature differences, keep the intended operating conditions with the drawing. The material name provides one input to the review. The finished section, surface condition, mechanical constraint and heating pattern also affect what the part experiences. Establish the relevant test on a representative installed configuration when the application calls for it. Carry the actual mounting condition and acceptance criteria into the approval record so any subsequent design change can be compared on the same basis.
For repeat review, record which attributes are requirements of the finished component and which are characteristics of the trial route. The material grade, fit and approved appearance may be specified outputs. The stock dimensions and intermediate operations describe how the approved sample was obtained. When either record changes, use the link between them to identify the checks affected by the revision. Include the measurement position and the approved sample reference so the decision can be reconstructed later.
Technical Takeaway
Start with the finished section and identify which features come from stock, which are created by forming and which are established by finishing. Use the glass grade, the mating part and the required appearance or optical function to define the review. Approve the critical interfaces on a sample in the same state and orientation as the intended assembly.
Frequently Asked Questions
Can borosilicate tube stock be used for a part that is no longer tubular?
Yes. Reheating and reshaping can produce a wider body, a shoulder or a different opening from the original tube. Use a section drawing of the finished part to define the wall and opening requirements for the new shape.
Does borosilicate specify a manufacturing process?
It specifies a family of glass materials. A particular component can use a retained stock shape, a reheated and reshaped section, or a mold-formed profile. The geometry, material specification, surface requirements and assembly determine the route to review.
Which dimensions should be checked after edge finishing?
Check the dimensions that the edge or its adjacent face controls, such as installed length, opening clearance and contact with a holder. Give the inspection reference and identify the final finishing condition in the drawing.
Can the same inspection approve the fit and the optical result?
Use the mounting drawing to verify seating and clearance. For a lens or diffusing component, define a separate lit appearance or optical test if the application requires it. Carry the same sample revision through the checks when comparing trial parts.
Review Your Borosilicate Part Drawing
Share the section drawing, required material, finished edge and surface conditions, and the mating component or mounting drawing. Identify the features that control fit, appearance or optical function so the team can review the route and sample requirements.
Share Your Section Drawing and Mounting Details
Technical note. The diagrams illustrate stock and design principles. The process video shows a specific production example. Confirm the grade, forming and finishing route, tolerances and acceptance conditions for the actual component.
 English