Direct Answer
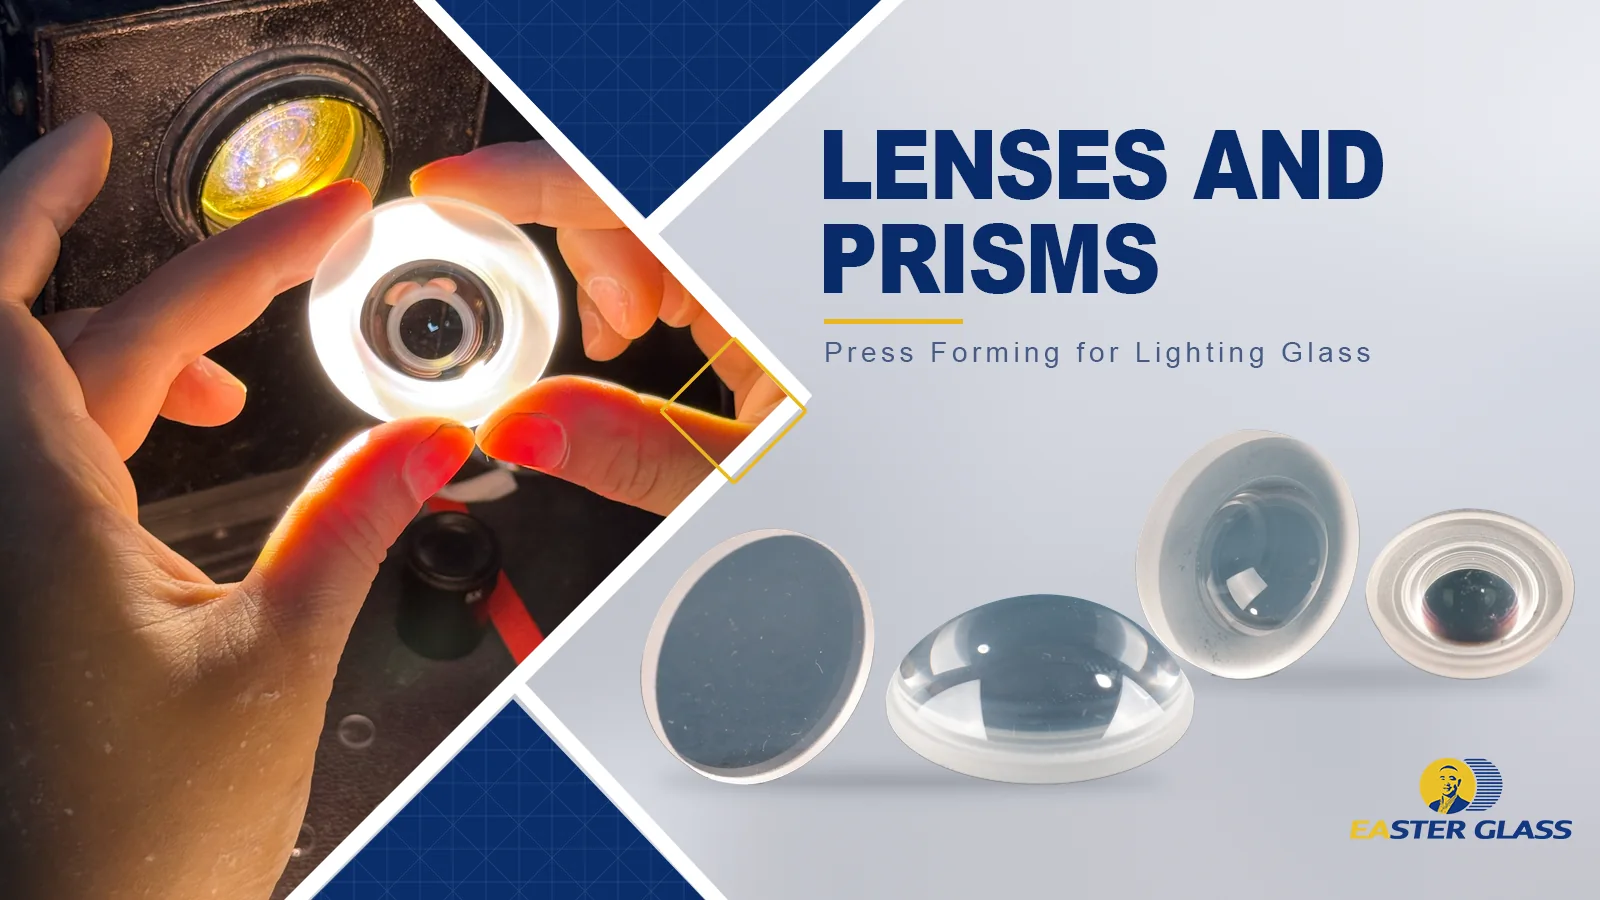
To make a pressed glass lens or prism, a press forces softened glass between shaped tool surfaces. The mold can form the lens profile, prism facets or texture, while cooling, release and any later finishing help determine the part that reaches inspection. For a lighting project, verify the formed surface, its position relative to the mounting features and its behavior in the intended assembly.
What does the glass press form?
A mold press shapes hot glass through contact with the tool. A plunger closes toward the cavity and displaces the softened glass into the space defined by the tooling. In a simple arrangement, the cavity and plunger can establish opposing faces, while a rim feature or separate ring can define the perimeter. The tool may therefore control a curved face, an array of raised features or a mounting rim in the same operation. The exact division of surfaces depends on the part and tool design. See the Corning Museum of Glass definition of mold pressing and the U.S. Department of Energy overview of glass press forming.
On a lighting drawing, separate the functional area of the glass from the surfaces used to locate, support or seal it. A ringed lens may need a specified step profile and a perimeter seat. A prism array may need facet directions referenced to an orientation feature. The location of the formed structure relative to the holder can matter as much as the structure itself. Mark the surfaces that the project expects to leave as formed and the features that will be inspected after later finishing. The broader choice between shaping a part with a press and shaping it by inflation is covered in the pressed-versus-blown lighting glass comparison.
What happens between the glass charge and the finished lens?
Prepare the glass and the tool
The starting form depends on the route. A charge can be a portion of hot glass delivered to the mold or a prepared piece of glass heated for forming. In optical molding literature, a prepared starting shape is called a preform. Its shape, surface and amount of glass matter because the tooling has to displace that material into the required form. Start a technical review by defining the intended glass grade and drawing revision, then ask which features are formed at the tool. The Borosilicate Glass collection for material-specific parts illustrates the separate material choice that can apply to a lighting component.
Press, cool and release the part
As the tool closes, the glass must reach the required regions of the cavity. A shallow face and a local groove impose different forming demands. Review narrow regions, abrupt transitions and the outer perimeter where a change in the hot glass, the tool condition or the trial setup can leave a feature incompletely defined. On a sample, identify which region differs from the drawing and compare parts at the same stage of the process. A mark that appears repeatedly at one position is a useful lead for examining that part of the tool, provided the inspection also accounts for handling and finishing.
The part needs enough shape stability for release and transfer. In general glass press forming, tool temperature and the time allowed for the glass to set affect the forming cycle. Further cooling and any applicable annealing need to suit the glass and geometry. Inspect the dimensions at the agreed cooled state, and record whether the sample is as pressed or has completed subsequent operations. For instance, a measured rim that will later be ground belongs to a different drawing state from the finished seating face. The DOE manufacturing profile describes these considerations in its general pressed-glass discussion.
Decide where finishing belongs
The term pressed glass lens describes a forming step. The drawing and process record should establish whether the functional surface stays as formed, whether a surface treatment is applied, and whether a separate edge or seat is ground after forming. For first-article review, label which face the appearance reference describes. If a specified treatment changes the look of a ring or prism field, compare the treated parts under the agreed inspection conditions. A clear trial can still answer questions about feature fill or profile before the finished appearance is approved.
Keep a clear record of the surfaces used as references at each stage. A tool trial might use the formed perimeter to locate a lens, while the finished product locates on a seat ground from a different face. A reading taken from the first reference cannot be compared directly with one taken from the second without establishing their relationship. Record both where the molded structure sits and how the finishing operation locates the part. This makes the finished inspection reproducible when the tool or fixture changes.
| Stage | What the stage controls | Project evidence |
|---|---|---|
| Glass preparation | Starting form and material for the chosen route. | Agreed glass grade and identified starting form. |
| Pressing | Shape of the surfaces in contact with the tool. | Drawing-defined profile and trial sample. |
| Cooling and release | Condition of the glass when the tool opens and the part is transferred. | Cooled sample with forming or release marks located. |
| Finishing where specified | Final edge, seating surface or specified face treatment. | Finished state identified on the sample record. |
| Inspection | Conformance to the drawing and the assembly requirement. | Profile, mounting and functional results where applicable. |
See a production example from Easter Glass
The official production clip shows the sequence from preparing and loading the glass to using the pressing tool. Use the clip to locate the forming step in the production sequence. A project drawing and representative samples establish which features the tool has to reproduce for that component. The wider lighting glass forming process overview puts pressing alongside the other routes used for lighting parts.
How do reheat pressing and precision glass molding differ?
In its optical-glass technical information, SCHOTT describes reheat pressing as a route in which a glass blank is reheated and pressed to a shape for later grinding and polishing. In that context, pressing establishes a useful blank geometry and downstream processing produces the required optical surfaces. The same technical bulletin describes precision molding with a prepared preform and a tool designed to create the intended optical geometry directly. These are documented routes in optical manufacturing. See SCHOTT TIE-40 on optical glass for precision molding.
A review of precision glass molding describes controlled heating, compression, cooling and demolding of an optical preform. The preform, mold and thermal cycle together affect the shape of the cooled part. This helps explain why the final form must be evaluated on a representative sample even when a drawing surface is intended to come from the mold. It also clarifies what to ask about a lighting part described as precision pressed. Identify the required surface, which step establishes it and the evidence that the finished part meets the drawing. See the review of precision glass molding for optical lenses.
On a lighting drawing, specify the profile needed in the fixture and document the proposed forming and finishing sequence for that design. If the functional geometry is formed in the mold, define how it will be measured after cooling and finishing. If later work establishes the surface, define the inspection state and datum for that work. Product pages may use the process label Precision Pressing. The label supports discussion of the stated forming route. Optical tolerances, the glass prescription and the specific manufacturing sequence depend on the project evidence.
Which features should the tool and the drawing agree on?
Fresnel rings and the seating rim
A stepped circular lens has a patterned zone and a perimeter used to place or retain the glass. The frosted borosilicate Fresnel lens with concentric steps gives a concrete example of these two areas. With a supplier of frosted borosilicate Fresnel lenses for spotlights, specify the face carrying the rings, the stepped region’s position relative to the seat, and the face or zone to be frosted. Show the section the team will use to review the steps. An outside diameter check alone covers one part of that drawing and leaves the ring geometry to a separate check.
Specify which sections of the profile are critical and where a transition or witness line is permitted. An oblique photograph is useful for documenting the presence and general layout of a ring pattern. Profile evidence calls for a drawing-defined section and an agreed measurement method. If the project changes the seat after the mold trial, recheck the position of the formed field relative to the final seat. The Optical Glass collection of lenses and light-control components provides related examples in which the optical face and mounting features serve different functions.
Prism facets and mounting orientation
A prismatic part carries repeating facets or relief that must be evaluated in the intended orientation. A useful drawing identifies the patterned face, the direction of the repeating features where relevant and the area that will remain visible after installation. Where facet angles or the edge of a pattern are critical, agree how to check them against the tooling and assembled part. Tool opening, parting and release need to be considered alongside the geometry so that any change to the profile receives an engineering review.
During custom mold design for prismatic lighting glass, show which profile features can move and which are controlled by the optical or assembly requirement. If the tool designer proposes a small transition at the end of a facet, locate it on the drawing and review whether it falls in the exposed field. The finished drawing can then identify a profile to inspect and a permitted edge transition. This is especially helpful when the part is handled by several teams during tooling, finishing and inspection.
For a factory pressing prismatic glass globes for decorative pendant luminaires, an integral neck gives the drawing team a reference for the mounting interface. The clear prismatic globe with an integral mounting neck illustrates a textured body and a fitting region on the same part. Describe the approved extent of the textured surface relative to the neck and holder. If the project requires a controlled rotational position, define an orientation reference in the assembly. For a decorative feature, document the agreed appearance in its intended setting.
Lens array pitch and registration
The borosilicate panel with repeated domed lens elements illustrates a formed array on a single glass component. When working with a manufacturer of press-molded glass lens arrays for LED luminaires, share the emitter layout and the mechanical reference for locating the glass. Define the position and spacing of the lens elements from that reference. For an array paired with a board, compare row or column spacing, the position of the first element and any offset or rotation between the two patterns.
An array can reproduce the repeated form and still sit in the wrong position relative to the emitters. The review should therefore cover the outline, seating surfaces, element locations and representative element profiles. If the drawing uses a key, corner or another locating feature, set that reference consistently for inspection. The pressed panel’s published geometry is a starting point for explaining how a mold reproduces repeated features. The hypothetical emitter arrangement illustrates how to define and check registration in a particular luminaire.
| Form | Tool-defined feature to review | Reference or assembly check |
|---|---|---|
| Stepped Fresnel lens | Concentric step profile and pattern boundary. | Section referenced to the finished perimeter seat. |
| Prismatic glass globe | Facet field and transition into the mounting region. | Neck position, exposed pattern and orientation in the holder. |
| Lens array panel | Repeated element profile and spacing. | Array origin, orientation and emitter alignment. |
What should a first-article review check?
Trace surface observations to the forming stage
The mold and glass touch during pressing, and the contact condition can influence the formed surface and how the part releases. A peer-reviewed study of the precision glass molding literature identifies adhesion at that interface as a contributor to surface quality and tool durability problems. Apply the diagnostic distinction carefully in a lighting review. Map the position of the observed mark and compare it with the tool, the release path and the areas handled or finished later. Confirm the cause with representative parts before accepting a correction. See the review of mold-glass interface adhesion.
A shallow facet, a mark that repeats in one cavity and a scratch that appears after finishing call for different follow-up. Keep the glass samples traceable to the relevant drawing revision, trial conditions and finishing state. If a surface difference appears across several parts, compare its position using the same drawing references and viewing conditions. That record allows the team to distinguish possible incomplete feature fill from a mark associated with release, the inspection setup or later handling. Use the Easter Glass quality guidance for inspection and acceptance samples to frame the project evidence.
Choose a profile check that reaches the feature under review. A measurement across the outer diameter or a contact reading on the tallest points can miss the valley of a stepped feature. If the profile matters, define the section, measurement direction and surfaces used to position the sample. Then ask for results that identify individual points or a profile trace, as appropriate to the drawing. Agree on a representative reference sample for appearance and keep the geometry criteria in the inspection record for the next tool trial.
Worked example of a panel that fits but is misaligned
Consider a rectangular glass lens array over an LED board in a housing. The outer edge fits the holder and the sample looks even at a glance. In the assembly, the last row of elements is offset from the corresponding emitters. Check which corner or seating face locates the glass, then measure the first and last rows from that reference. Compare the board position in the same fixture. If the first row aligns and the difference grows across the panel, check element spacing. If the rows shift together by a similar amount, check the overall array position and the assembly references.
Record the observed direction and location of the difference with a sample identifier. Repeat the check at the intended assembly orientation and finished state, including any operation that changes a seating surface. If an optical outcome is specified, review the agreed assembled test after confirming the physical position. That sequence helps distinguish a tooling or drawing issue from a board or holder issue. Record the geometry check and the functional check as separate results so that a pass on one requirement can be interpreted correctly.
Put the acceptance inputs on the drawing
Include the material requirement, functional surface, applicable pattern or profile, and the seating and orientation references. Define the inspection state and representative fixture before approving the first article. Where a finish or parting line is visible, identify its allowable region and the method for judging it. For made-to-drawing glass lens prototypes, share the drawing revision and the mating part or assembly view. The Easter Glass drawing and tooling development process provides the project route for reviewing those inputs before tool and sample decisions.
Technical Takeaway
Start with a section that identifies the formed optical or textured surface and the surfaces that locate the glass. Agree on the state in which the part will be measured, the reference for its pattern or profile and the assembly check that verifies its role. Use the tool trial to document feature reproduction, then check the cooled, finished part against the drawing. Apply the result to the component, glass and tool that the sample represents.
Frequently Asked Questions
How is a pressed glass lens made?
Softened glass is placed in the forming tool and shaped as the press closes. The part is cooled and released, then finished if the design requires additional work. First-article review checks the required profile, seating features and surface condition at the agreed stage.
What is the difference between reheat pressing and precision glass molding?
In the optical-glass context described in TIE-40, reheat pressing produces a shaped blank whose optical surfaces are finished in later steps. Precision glass molding uses a prepared preform and controlled tooling to form the intended optical surface. A lighting project needs the actual forming and finishing sequence for its design.
Which lighting structures are made by pressing?
Published examples include concentric stepped Fresnel lenses, prismatic surfaces and panels with repeated domed lens elements. Their suitability for pressing depends on the glass, tool access, release and the finished features required. Specify the geometry and inspect it in the intended assembly.
Why does the mold matter for a pressed prism or lens?
The tool defines the surfaces it contacts, including the profile or texture where those features are mold formed. The final result also depends on glass condition, cooling, release and finishing. Evaluate a drawing-defined profile and inspect the agreed locations on finished samples.
Review Your Pressed Lens or Prism Drawing
Share the drawing, glass requirement, functional face and mounting references. Include the light-source layout or a representative assembly if it determines alignment. Mark the features that need to be reproduced by the mold and the checks required on the finished part.
Share Your Lens or Prism Drawing
Technical note. The diagrams illustrate general forming and inspection concepts. The public product examples describe their listed geometry, material where stated and process labels. Confirm the glass grade, tooling, finished tolerances and optical requirements for the actual project.
 English